Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
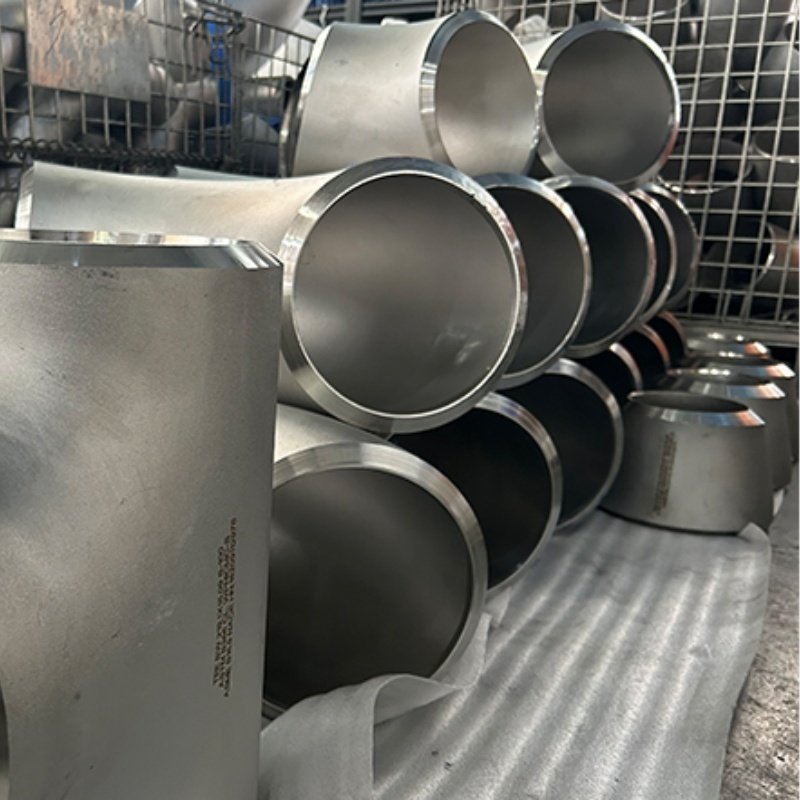
Super austenitic stainless alloys UNS N08926 and N08925 sit between the standard 6-molybdenum austenitic grades and super duplex stainless steels. Both carry roughly 6% molybdenum with 24-26% nickel, giving pitting resistance close to super duplex while retaining the formability and weldability of austenitic material. This page covers the butt weld fitting product form manufactured to ASME SB-366 for these two grades, and what a buyer needs to state on the purchase order to get the correct material.
ASME SB-366 covers factory-made wrought nickel and nickel alloy fittings, and Table 2 lists UNS N08925 and N08926 as permissible fitting grades. Their raw material options are broad:
Forged flanges and forged fittings in the same grades are covered by ASME SB-462. Flat product tolerances follow ASME B906.
| Grade | UNS | Ni | Cr | Mo | Fe | Key Characteristic |
|---|---|---|---|---|---|---|
| Alloy 926 (6% Mo super austenitic) | N08926 | 24.00-26.00 | 19.00-21.00 | 6.00-7.00 | remainder | Highest pitting resistance in the austenitic family |
| Alloy 925 (low C, Cu-bearing) | N08925 | 24.00-26.00 | 19.00-21.00 | 6.00-7.00 | remainder | Lower carbon for improved weldability |
| Alloy 31 (N08031) | N08031 | 30.0-32.0 | 26.0-28.0 | 6.00-7.00 | remainder | Higher Ni and Cr, N-bearing |
| Alloy 66 / 67 | N08366 / N08367 | 23.50-25.50 | 20.00-22.00 | 6.00-7.00 | remainder | Matching 6% Mo seamless pipe |
| Element | UNS N08925 (%) | UNS N08926 (%) | Limit Type |
|---|---|---|---|
| Carbon | 0.020 max | 0.020 max | max |
| Manganese | 1.00 max | 2.00 max | max |
| Phosphorus | 0.045 max | 0.03 max | max |
| Sulfur | 0.030 max | 0.01 max | max |
| Silicon | 0.50 max | 0.5 max | max |
| Nickel | 24.00-26.00 | 24.00-26.00 | range |
| Chromium | 19.00-21.00 | 19.00-21.00 | range |
The tighter sulfur limit of 0.01% max on N08926 is the principal difference between the two grades in SB-625 Table 1. In SB-366 Table 2, N08925 is listed as CR1925 / WP1925 and N08926 as CR1925N / WP1925N.
| Alloy | UNS | Heat Treatment, °F [°C] | Quench |
|---|---|---|---|
| Alloy 925 (low C-Ni-Fe-Cr-Mo-Cu) | N08925 | 1800-1900 [983-1038] | Rapid Air/Water |
| Alloy 926 (low C-Ni-Fe-Cr-Mo-Cu-N) | N08926 | 2150 [1177] | Rapid Air/Water |
The two grades are not interchangeable on heat treatment: N08925 carries a 1800-1900°F range while N08926 is treated at 2150°F. Specify the UNS number on the order rather than a trade name so that the mill applies the correct cycle.
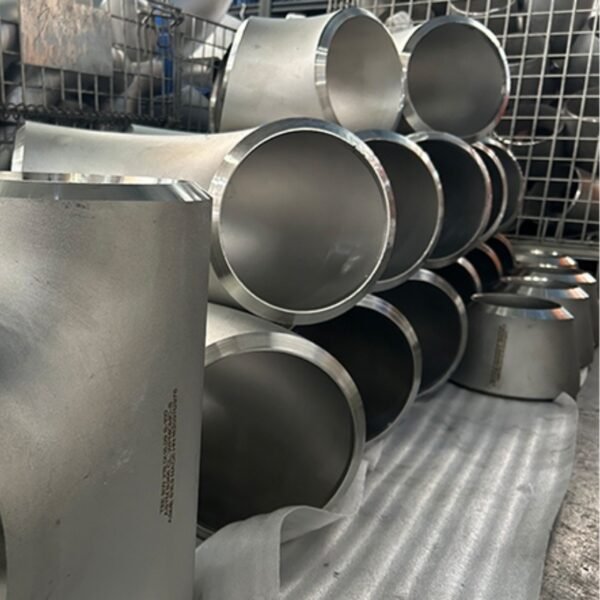
Butt weld fittings are supplied in ASME B16.9 geometry, covering elbows (45°, 90°, 3D and long-radius), equal and reducing tees, concentric and eccentric reducers, and caps. Pressure class availability follows the B16.9 class table; specify the class on the order line. For socket weld and threaded patterns, refer to ASME B16.11. Wall thickness and weights are theoretical values derived from the applicable B16.9 dimensional tables.
These grades are selected where chloride pitting and crevice corrosion control the design rather than chloride stress corrosion cracking resistance alone. Typical service environments include:
Orders are supplied with a mill test certificate per EN 10204 3.1 unless otherwise specified. Available inspection items include:
Please include the following when requesting a quotation:
Send the specification you are working to and the service conditions, and we will confirm the grade, dimensions and availability along with an FOB quotation.
Related specifications and products. Super austenitic N08926 and N08925 butt weld fittings are supplied alongside the duplex ranges. See the nickel alloy butt weld fitting range super duplex 2507 butt weld fittings duplex 2205 butt weld fittings for the dimensional and material basis behind this page.