Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
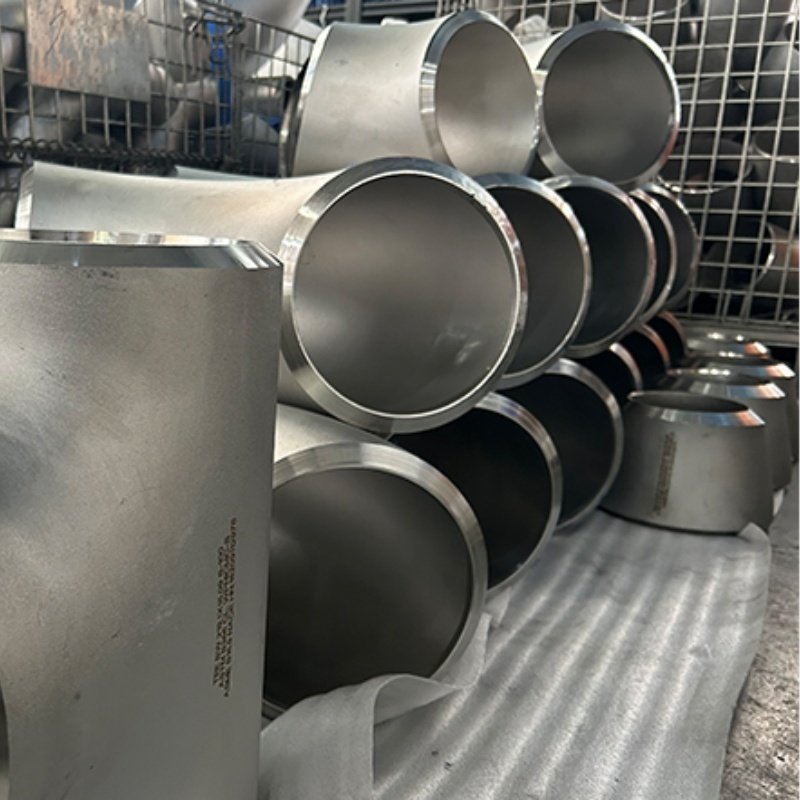
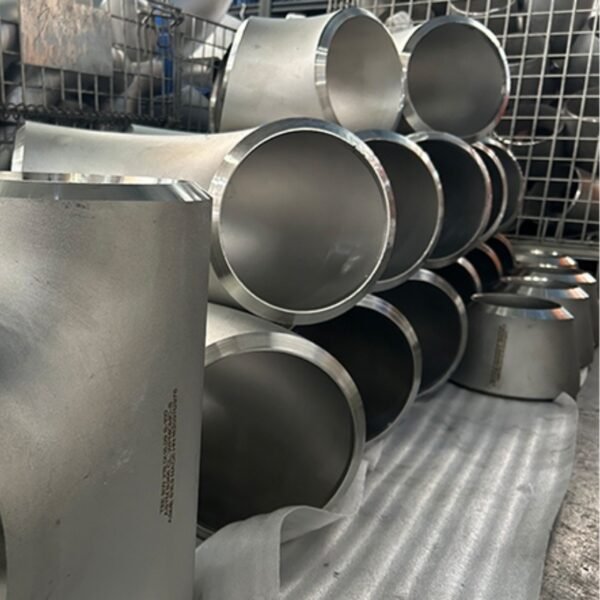
Super Duplex 2507 butt weld fittings to ASME B16.9 and SA-182 F 53 / F 55. UNS S32750 and S32760, solution annealed and quenched. EN 10204 3.1 MTC.
Super Duplex 2507 butt weld fittings are the high-chromium, high-nitrogen members of the duplex family, used where 2205 is no longer enough: hot seawater and splash zones, acidified produced water, sour service with chlorides, and the mineral acid and pulp bleaching plant applications that punish 22 % chromium. Two forging grades carry the name. F 53 in UNS S32750 reaches its pitting resistance with chromium, molybdenum and nitrogen alone, while F 55 in UNS S32760 adds copper and tungsten for better behaviour in reducing acids and in crevices. Both are supplied solution annealed and quenched, and both are supplied to ASME B16.9 dimensions so that they match the pipe they are welded to and can be examined as a full-penetration joint.
For the full range of butt weld forms in stainless and nickel alloy see our nickel alloy butt weld fittings overview, and for the matching pipe see nickel alloy pipe and tube. The grade selection map for duplex and super duplex is on our duplex stainless steel fittings page on the pipe and tube site.
| Designation | Value |
|---|---|
| Forging grades | ASME SA-182 F 53 (UNS S32750) and F 55 (UNS S32760) |
| Wrought fitting grades | ASME SA-815 WPS32750 / CRS32750 and WPS32760 / CRS32760 |
| Dimensional standard | ASME B16.9 (factory-made wrought buttwelding fittings) |
| Heat treatment | Solution treated and quenched; F 53 at 1880 °F (1025 °C) minimum, F 55 at 2010 to 2085 °F (1100 to 1140 °C), liquid quench |
| Preheat and post-weld heat treatment | Neither required for the ferritic-austenitic grades in ASME SA-182 |
| Weld metal | Deposited weld to conform to the base metal composition; no exception is listed for UNS S32750 or UNS S32760 in ASME SA-815 |
| Delivery condition | Solution treated, quenched and pickled |
| Element | F 53 (S32750), % | F 55 (S32760), % |
|---|---|---|
| Chromium | 24.0 – 26.0 | 24.0 – 26.0 |
| Nickel | 6.0 – 8.0 | 6.0 – 8.0 |
| Molybdenum | 3.0 – 5.0 | 3.0 – 4.0 |
| Nitrogen | 0.24 – 0.32 | 0.20 – 0.30 |
| Tungsten | no requirement | 0.50 – 1.00 |
| Copper | 0.50 | 0.50 – 1.00 |
| Carbon | 0.030 | 0.030 |
| Manganese | 1.20 | 1.00 |
| Silicon | 0.80 | 1.00 |
| Phosphorus | 0.035 | 0.030 |
| Sulfur | 0.020 | 0.010 |
Composition as published in ASME SA-182 Table 2 for F 53 and F 55. The tungsten and copper columns are what separate F 55 from F 53 chemically, and they are the reason the two grades are not simply a heavier and a lighter version of the same thing. ASME SA-815 lists the equivalent wrought grades for the same UNS numbers.
| Grade | Tensile, min ksi (MPa) | Yield (0.2 %), min ksi (MPa) | Elongation, min % | Hardness, max HBW |
|---|---|---|---|---|
| F 53 (S32750) | 116 (800) | 80 (550) | 15 | 310 |
| F 55 (S32760) | 109 – 130 (750 – 895) | 80 (550) | 25 | no limit |
As published in ASME SA-182 Table 3. Two points are worth noticing before the order is written. The hardness limit of 310 HBW applies to F 53 only, so the two grades are treated differently by the specification itself. And F 55 is published with a tensile strength range rather than a single minimum, so the certificate for a F 55 fitting shows a band, not a floor. ASME SA-182 also lists a minimum elongation of 15 % for F 53 against 25 % for F 55, which matters when the fitting has to be formed or expanded after delivery.
| Item | Requirement |
|---|---|
| Governing dimensional standard | ASME B16.9 |
| Nominal size range covered | NPS 1/2 to NPS 48 (DN 15 to DN 1200) |
| Wall thickness | As the pipe schedule to which the fitting is welded |
| End preparation | Bevelled to ASME B16.25, plain ends on request |
| Common forms | 90° and 45° elbows, 180° returns, tees, crosses, concentric and eccentric reducers, caps, couplings and lap joint stub ends |
| Mating flange | ASME B16.5 up to NPS 24, ASME B16.47 for the larger sizes, in the matching forging grade |
| Availability beyond the standard range | TBC against the specific enquiry |
Forged super duplex fittings are hot worked and then solution treated and quenched. ASME SA-182 Table 1 requires F 53 to be solution treated and quenched at 1880 °F (1025 °C) minimum with liquid quenching, and F 55 at 2010 to 2085 °F (1100 to 1140 °C), also liquid quenched. The higher temperature band for F 55 follows from the copper and tungsten additions, and it is one of several reasons the two grades should not be interchanged without checking the certificate. The wrought grades to ASME SA-815 are solution treated in their own bands, 1920 to 2060 °F (1025 to 1125 °C) for UNS S32750 and 2010 to 2085 °F (1100 to 1140 °C) for UNS S32760, with no tempering required. As with all duplex material, the quench through the intermediate range is what preserves the phase balance, the toughness and the corrosion resistance together.
Fittings are supplied solution annealed and pickled, with a machined surface
finish. Each fitting carries the grade, the governing material specification, the
dimensional standard, the nominal size and the heat number, linked to the
EN 10204 certificate issued with the shipment. Export packing is by wooden
crate, steel pallet or case, with plastic end caps and, where required, VCI
protection inside the case. Beveled or plain ends are confirmed with the
order. Delivery schedule, quantity, minimum order quantity and price are
confirmed only against a specific enquiry.
2507 is bought for pitting resistance, and that is a nitrogen argument. The step from 2205 to super duplex is not mainly chromium, which is already 24 to 26 % in both grades. It is molybdenum, nitrogen and, in F 55, tungsten and copper. Nitrogen is the most efficient pitting resistance element per unit of cost, and it is also the element that stabilises the austenite phase. The higher nitrogen range of F 53, 0.24 to 0.32 %, is the reason the grade reaches its pitting resistance with a slightly higher tensile floor and a noticeably lower minimum elongation than F 55. Grade selection is therefore a trade between pitting margin and formability, and it should be made explicitly rather than by default.
Super duplex has the narrowest process window in the stainless family. The precipitation of sigma, chi and chromium nitride phases in the intermediate range is the dominant failure mode, and it takes both chemistry and cooling rate to suppress it. That is why the specification pins the solution annealing temperature to a narrow band and requires liquid quenching, and why the heat treatment must be completed before any machining, so that the material is not re-stressed or re-heated afterwards. A super duplex fitting that has been welded to and then slowly cooled on the shop floor is not a super duplex fitting any more, and the certification route has to reflect the real thermal history.
Weld metal has to match the base metal, with no exception for these grades. ASME SA-815 lists exceptions for a small number of grades, and UNS S32750 and UNS S32760 are not among them, so the deposited weld has to conform to the base metal composition. Reproducing the nitrogen, and the copper and tungsten of F 55, in the weld metal is the constraint that narrows consumable selection, and it is why the filler specification belongs in the purchase order and the welding procedure qualification, not in the welding shop’s discretion.
Cost pressure usually decides the grade before metallurgy does. Super duplex exists because the service demanded it, and it is tempting to step down to 2205 when a line is re-tendered. That substitution is only defensible with corrosion data for the actual service, because the gap between the two grades widens precisely in the conditions where super duplex was specified: hot seawater, acidified brine and tight crevices. Where the grade has been downgraded, the corrosion allowance and the qualification have to be revisited rather than carried across.
F 53 is UNS S32750 and reaches its pitting resistance with chromium, molybdenum and nitrogen, giving a 116 ksi tensile minimum with 15 % elongation and a 310 HBW hardness limit. F 55 is UNS S32760 and adds 0.50 to 1.00 % tungsten and 0.50 to 1.00 % copper, giving a 109 to 130 ksi tensile band with 25 % elongation and no hardness limit.
Solution treated and quenched with liquid quenching: F 53 at 1880 °F (1025 °C) minimum and F 55 at 2010 to 2085 °F (1100 to 1140 °C), per ASME SA-182 Table 1. The quench rate through the intermediate range is what preserves the phase balance.
No. ASME SA-182 requires neither preheat nor post-weld heat treatment for the ferritic-austenitic grades. Heat input control and a qualified filler protect the joint instead.
ASME SA-815 requires the deposited weld to conform to the base metal composition, and lists no exception for UNS S32750 or UNS S32760, so the consumable has to reproduce the nitrogen and, for F 55, the copper and tungsten.
Yes, that is the principal application for the grade. Seawater lift, injection, firewater and cooling systems offshore are typically specified in super duplex for exactly this duty, and the qualification should be against corrosion data for the actual temperature, chlorides and crevice geometry.
ASME B16.9 covers NPS 1/2 to NPS 48, DN 15 to DN 1200, with the fitting wall following the pipe schedule. Specific availability is confirmed against the enquiry.