Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
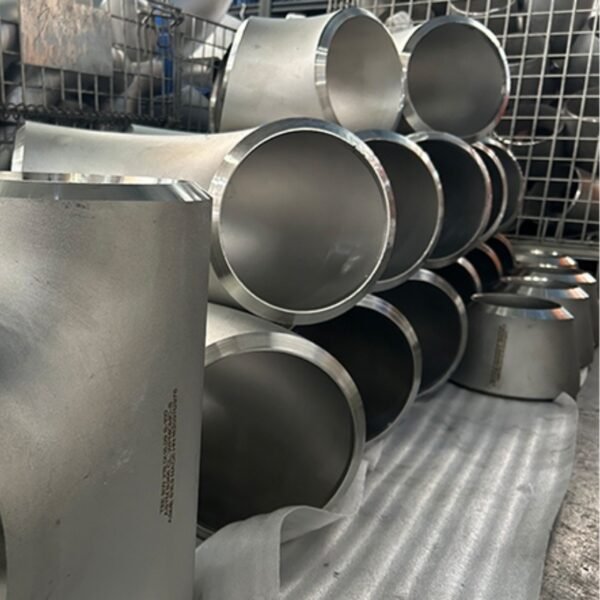
The table below sets out the governing material specification and the grade comparison for Hastelloy B (Alloy B) UNS N10001 Butt Weld Fittings. All composition and mechanical values are taken directly from the ASME BPVC Section II specifications named in each row.
| Grade | UNS | Ni | Mo | Cr | Fe | C max | Heat treatment |
|---|---|---|---|---|---|---|---|
| Alloy B | N10001 | rem. | 26.0–30.0 | 1.0 max | 4.0–6.0 | 0.05 | 1950 °F [1065 °C] min, rapid air/water |
| Alloy B-2 | N10665 | rem. | 26.0–30.0 | 1.0 max | 2.0 max | 0.02 | 1950 °F [1065 °C] min, rapid air/water |
| Alloy B-3 | N10675 | 65.0 min | 27.0–32.0 | 1.0–3.0 | 1.0–3.0 | 0.01 | 1950 °F [1065 °C] min, rapid air/water |
| Alloy B-4 | N10629 | rem. | 26.0–30.0 | 0.5–1.5 | 1.0–6.0 | 0.01 | 1975 °F [1080 °C], rapid air/water |
We supply Hastelloy B butt weld elbows (45° and 90°), concentric and eccentric reducers, equal and reducing tees, 180° return bends, caps, crosses and lap joint stub ends. Dimensions follow ASME B16.9 for butt weld forms and ASME B16.11 for socket weld and threaded forms, with MSS SP-43, SP-95 and SP-97 available on enquiry. Size and wall thickness availability depend on plate and forging stock, so confirm the specific size and schedule against our current stock before ordering.
Hastelloy B fittings are produced under ASME SB-366 from raw material meeting ASME SB-333 (plate, sheet and strip) or ASME SB-335 (rod and bar), with forgings to ASME SB-564. All fittings are furnished heat treated and rapidly quenched. Welding consumables, filler metal selection and the weld procedure for welded construction are agreed with the purchaser, since the alloy content of deposited weld metal must conform to the base metal per SB-366 §6.4.
Records of chemical analysis made in accordance with the applicable material specification are the certification that the fitting meets SB-366 requirements. Test reports are required for all fittings covered by SB-366 and shall include the specification year-date and class, heat numbers traceable to heat numbers, chemical analyses and mechanical properties for all starting materials, weld metal analyses or AWS classification where filler metal was added, the heat treatment applied, results of all nondestructive examinations, and a statement that the fitting was manufactured, sampled, tested and inspected in accordance with the specification.
| Item | Requirement |
|---|---|
| Material specification | ASME SB-366 (wrought nickel and nickel alloy fittings) |
| Dimensional standard | ASME B16.9 (butt welding) / ASME B16.11 (socket weld and threaded) |
| Material designation | CR HB (corrosion resistant) / WP HB (pressure fitting), UNS N10001 |
| Heat treatment | 1950 °F [1065 °C] minimum, rapid air or water quench |
| Fitting construction classes | S seamless, W welded (RT or UT), WX welded radiography, WU welded ultrasonic |
| Marking | Manufacturer, material, grade, size, schedule, and CR or WP designation per SB-366 §13.1 |
Chemical composition shall conform to the applicable ASME specification. The table below reproduces the composition limits for the grades covered by Hastelloy B (Alloy B) UNS N10001 Butt Weld Fittings.
| Element | Composition, % (ASME SB-333 / SB-335 Table 1) |
|---|---|
| Nickel | Remainder |
| Molybdenum | 26.0–30.0 |
| Iron | 4.0–6.0 |
| Chromium | 1.0 max |
| Carbon, max | 0.05 |
| Silicon, max | 1.0 |
| Cobalt, max | 2.5 |
| Manganese, max | 1.0 |
| Alloy (SB-335 Table 3) | Thickness, in. (mm) | Tensile min, psi (MPa) | Yield min, psi (MPa) | Elongation min, % |
|---|---|---|---|---|
| N10001 | 5/16 to 3 1/2 (7.94–38.1) incl. | 115 000 (795) | 46 000 (315) | 35 |
| N10001 | Over 3 1/2 to 3 1/2 (38.1–88.9) incl. | 100 000 (690) | 46 000 (315) | 30 |
The primary application. Molybdenum content carries the alloy in reducing HCl, and the absence of chromium avoids the pitting and intergranular attack mechanisms that limit chromium-bearing nickel alloys. Pumps, columns and reactor nozzles handling dechlorination and acid regeneration streams are typical installations.
Hastelloy B is widely used in sulphuric acid and in phosphoric acid evaporation where reducing conditions and chloride carry-over are present. Sparger piping and agitator shaft sleeves in phosphoric acid concentrators use this grade.
Acetic acid, formic acid and organic acid intermediates in the petrochemical and pharmaceutical industries are common service environments for Alloy B components, particularly in absorber and knockout sections where trace chloride is present.
Because the alloy is free of chromium it does not form a protective chromium oxide film, so it is generally not a first choice for oxidising or high-temperature service. Where vacuum duty requires a low-outgassing nickel-based material, Hastelloy B is specified in specific applications — check the temperature and atmosphere limits with our technical department before finalising a grade selection.
Full analysis to the limits of the applicable raw material specification, with product (check) analysis available on order.
Solution heat treated to SB-366 Table 3 with rapid air or water quench, and the treatment recorded on the test report.
One tension test per lot on one fitting or a representative test piece from the same heat, heat treated in the same batch or charge. Test reports state whether tension testing was performed.
Class S requires no NDE. Class W is radiography or ultrasonic. Class WX requires radiography of all welds; Class WU requires ultrasonic of all welds.
Sizes, shapes and dimensions in accordance with ASME B16.9, ASME B16.11 and the applicable MSS SP documents.
Available on order as a supplementary requirement under SB-366 Supplementary Requirement S6, with 100 % of product examined per Guide E1916.
Available on order under SB-366 Supplementary Requirement S3, all surfaces tested to Practice E165 with acceptance limits as specified by the purchaser.
Not required by SB-366. Fittings shall be capable of withstanding the test pressure prescribed in the specification for the pipe with which the fitting is used. A hydrostatic test may be applied as agreed between manufacturer and purchaser under Supplementary Requirement S4.
Send us the grade, product form, nominal size, wall thickness or schedule, quantity, and the service conditions including concentration, temperature and pressure. We will confirm dimensional compliance to ASME B16.9 or B16.11, the material route and available delivery schedule, and issue a quotation on request. For items requiring positive material identification, liquid penetrant examination or a specific test report format, state these with the enquiry so they are included in the order.