Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Incoloy 800, 800H and 800HT butt weld fittings to ASME SB-564 and B16.9. Ni-Fe-Cr alloy for furnace parts, heat exchangers and carburising service.
Incoloy 800, 800H and 800HT are the three UNS-registered variants of the same nickel-iron-chromium family, differentiated by grain size and carbon control rather than by base chemistry. Tailan Metal supplies all three as butt weld fittings to ASME SB-564 for material and ASME B16.9 for dimensions, plus forging stock for fabricators who machine their own components.
| Grade | UNS | Service temperature | Distinguishing feature |
|---|---|---|---|
| Incoloy 800 | N08800 | up to 1100 degF (593 degC) | Standard annealed grain size |
| Incoloy 800H | N08810 | above 1100 degF (593 degC) | Controlled grain size for creep and rupture |
| Incoloy 800HT | N08811 | above 1100 degF (593 degC) | Fine grain, higher creep-rupture strength |
| Incoloy 825 | N08825 | similar envelope | Molybdenum and copper for reducing and acid service |
ASME SB-564 para. 1.1.1 states that UNS N08800 is normally employed in service temperatures up to and including 1100 degF (593 degC), while UNS N08810, N08120 and N08811 are normally employed above that range where resistance to creep and rupture is required, annealed to develop controlled grain size.
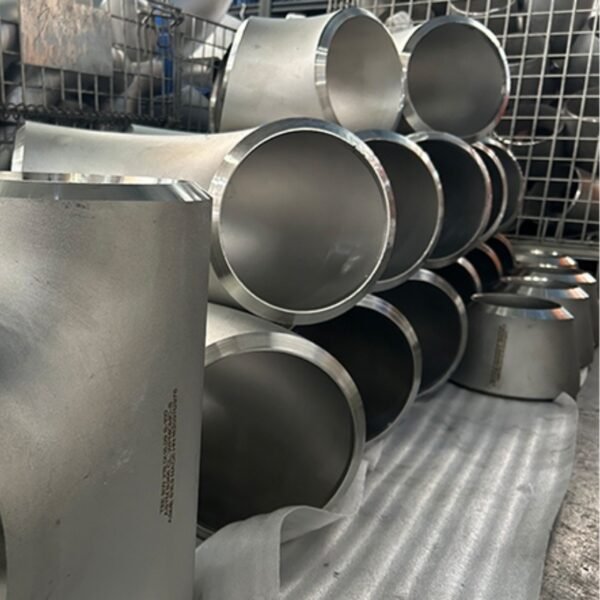
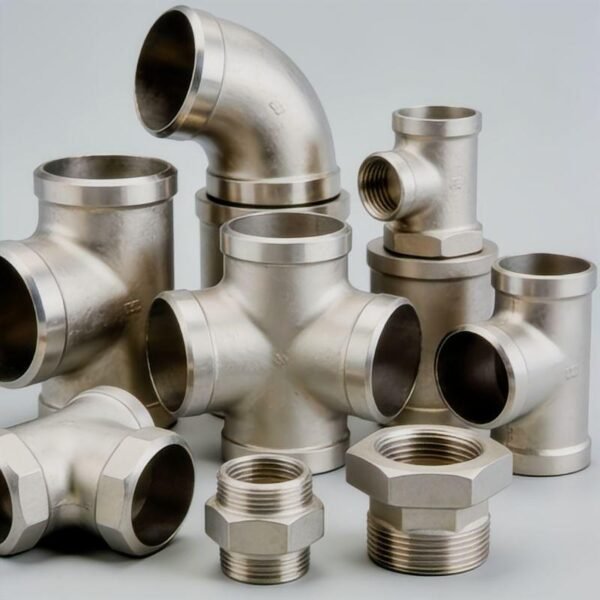
90 and 45 degree long-radius butt weld elbows, concentric and eccentric reducers, equal tees, reducing tees, caps, 180 degree return bends and lap-joint stub ends. Sizes DN 15 to DN 600, schedules to suit the customer drawing. Material supplied annealed per SB-564; forged bar and forging stock available for machined fittings.
| Element | N08800 | N08810 | N08811 |
|---|---|---|---|
| Nickel | 30.0-35.0 | 30.0-35.0 | 30.0-35.0 |
| Iron | 39.5 min (by difference) | 39.5 min | 39.5 min |
| Chromium | 19.0-23.0 | 19.0-23.0 | 19.0-23.0 |
| Carbon | 0.10 | 0.05-0.10 | 0.06-0.10 |
| Aluminium | 0.15-0.60 | 0.15-0.60 | 0.15-0.60 |
| Titanium | 0.15-0.60 | 0.15-0.60 | 0.15-0.60 |
| Manganese | 1.5 | 1.5 | 1.5 |
| Silicon | 1.0 | 1.0 | 1.0 |
| Sulfur | 0.015 | 0.015 | 0.015 |
| Copper | 0.75 | 0.75 | 0.75 |
| Grade | Tensile min | Yield min | Elongation in 2 in. min |
|---|---|---|---|
| UNS N08800 | 75 ksi (517 MPa) | 30 ksi (207 MPa) | 30% |
| UNS N08810 / N08811 | 65 ksi (448 MPa) | 25 ksi (172 MPa) | 30% |
Note the inverse relationship: 800H and 800HT trade a lower room-temperature tensile minimum for refined grain control that raises creep-rupture performance at elevated temperature. Grade selection must follow the design code, not the highest strength number.
Heat-treatment furnace fixtures and retorts, radiant tubes, heat exchanger shells and tube sheets, carburising and nitriding equipment, ethylene cracker transfer line systems, and petrochemical furnace manifolds.
EN 10204 3.1 / 3.2 certification, grain size verification to ASTM E112 when 800H or 800HT is ordered, hydrostatic shell test, PMI, and heat-number traceability on every fitting. Material marking per SB-564 para. 15 including alloy designation, specification number, heat number and condition.
Please specify grade (800 / 800H / 800HT), nominal size, schedule or wall thickness, quantity, and whether EN 10204 3.1 or 3.2 certification is required. Send drawings for non-standard items. We will confirm availability, grain-size compliance and lead time in the quotation.