Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
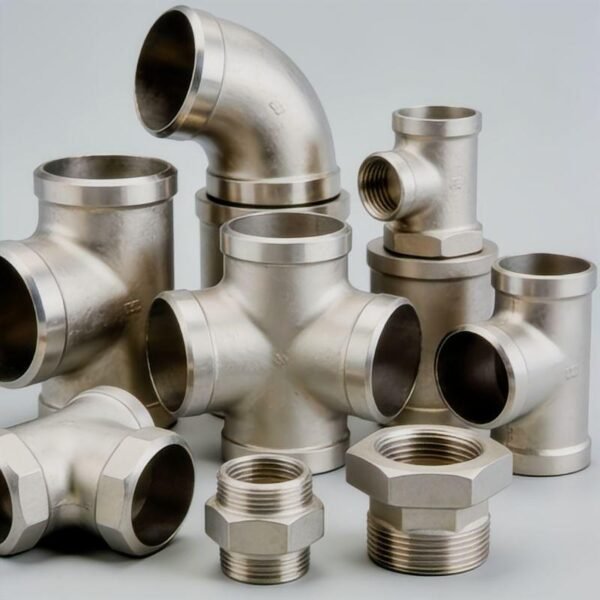
Hastelloy C-276 butt weld fittings (UNS N10276) forged to ASME SB-564 and dimensioned to ASME B16.9. With 16% chromium, 16% molybdenum and 4% tungsten, this is the general purpose corrosion workhorse for both reducing acids such as hydrochloric and sulphuric, and oxidising media such as wet chlorine, hypochlorite and nitric acid.
This page covers the alloy dimension. For the full range of butt weld fitting forms in any nickel alloy, see our nickel alloy butt weld fittings overview.
| Designation | Value |
|---|---|
| UNS number | N10276 |
| Material specification | ASME SB-564 (Nickel Alloy Forgings) |
| Dimensional standard | ASME B16.9 |
| Material class | Low-carbon nickel-chromium-molybdenum-tungsten |
Note on specifications: SB-564 is the correct ASME Section II specification for forged nickel alloy fittings. SA-182 covers low alloy and stainless steel only and does not include any nickel alloy grades.
| Fitting | Types |
|---|---|
| Socket weld elbow | 45°, 90°, 180° / reducing |
| Socket weld tee | Equal and reducing, straight and branch |
| Socket weld cross | Equal and reducing |
| Socket weld reducer | Concentric and eccentric |
| Socket weld coupling | Standard |
| Socket weld cap | Standard and heavy |
| Plug | Square head and hex head |
| Element | Composition, % | Element | Composition, % |
|---|---|---|---|
| Nickel | Remainder | Carbon | 0.010 max |
| Chromium | 14.5 – 16.5 | Silicon | 0.08 max |
| Molybdenum | 15.0 – 17.0 | Cobalt | 2.5 max |
| Tungsten | 3.0 – 4.5 | Manganese | 1.0 max |
| Iron | 4.0 – 7.0 | Vanadium | 0.35 max |
| Phosphorus | 0.04 max | Sulfur | 0.03 max |
Limits from ASME SB-622 Table 1. The very low carbon and silicon maxima are the signature of this alloy and are why it needs no post-weld heat treatment.
| Property | Typical requirement |
|---|---|
| Tensile strength | Specified on order, typically ≥ 100 ksi |
| Yield strength | Specified on order |
| Elongation | ≥ 35% typical |
| Grain size | ASTM E112 as agreed |
Fittings are supplied solution annealed and pickled, with a bright annealed or pickled surface as required. Each fitting carries heat number, grade, standard, size, heat treatment condition and our works mark. Export packing in wooden cases or steel pallets with plastic end caps.
Send the grade, fitting type, nominal size, schedule, quantity and any third-party inspection requirement to our technical sales desk. We will confirm dimensional tolerance, delivery condition and the applicable ASME line item, and quote FOB Shanghai or Ningbo.
B-2 performs better in strong reducing acid but its higher carbon and silicon make it susceptible to intergranular attack in the weld heat-affected zone, so it must be solution annealed after welding. C-276 with its very low carbon and silicon can be welded and put into service with no post-weld heat treatment, which usually decides the choice on fabrication cost alone.
C-22 has more chromium and less molybdenum, which gives better resistance to strongly oxidising acids such as nitric. If your service is oxidising-acid dominant, C-22 is the better choice; for everything else C-276 is the safer default.
It resists seawater, but for high-velocity seawater with entrained sand or oxidising biocides, Inconel 625 or titanium gives more pitting margin. C-276 is chosen where acids are present alongside chlorides.
Yes, as standard. We can also run ASTM G28 intergranular corrosion tests matching the service and issue the results with the certificate.