Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
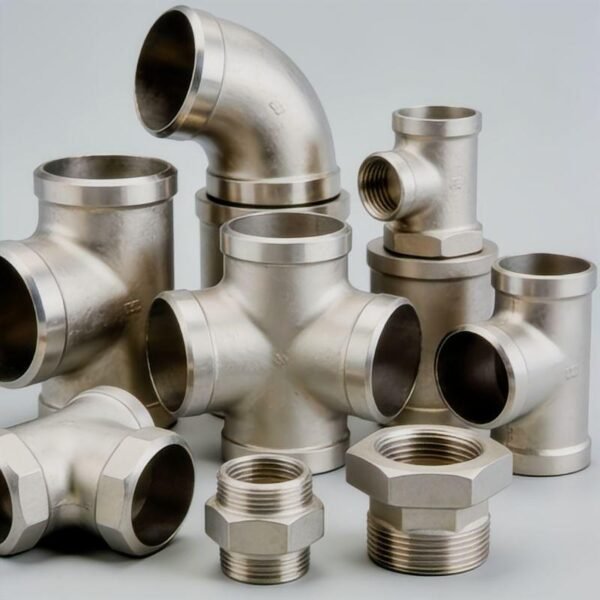
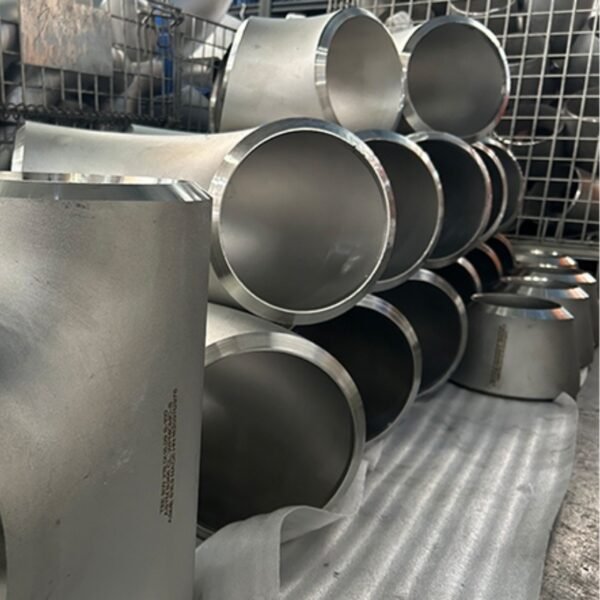
Inconel 625 socket weld fittings (UNS N06625) forged to ASME SB-564 and dimensioned to ASME B16.11. Socket weld is preferred over butt weld for small bore, high pressure and instrument lines where access to the pipe ID is limited.
This page covers the alloy dimension. For the full range of socket weld fitting forms in any nickel alloy, see our nickel alloy socket weld fittings overview.
| Designation | Value |
|---|---|
| UNS number | N06625 |
| Material specification | ASME SB-564 (Nickel Alloy Forgings) |
| Dimensional standard | ASME B16.11 |
| Material class | Nickel-chromium-molybdenum-columbium |
Note on specifications: SB-564 is the correct ASME Section II specification for forged nickel alloy fittings. SA-182 covers low alloy and stainless steel only and does not include any nickel alloy grades.
| Fitting | Types |
|---|---|
| Socket weld elbow | 45°, 90°, 180° / reducing |
| Socket weld tee | Equal and reducing, straight and branch |
| Socket weld cross | Equal and reducing |
| Socket weld reducer | Concentric and eccentric |
| Socket weld coupling | Standard |
| Socket weld cap | Standard and heavy |
| Plug | Square head and hex head |
| Element | Composition, % | Element | Composition, % |
|---|---|---|---|
| Nickel | Remainder | Carbon | 0.10 max |
| Chromium | 21.5 min | Manganese | 0.50 max |
| Molybdenum | 8.0 min | Silicon | 0.50 max |
| Niobium (Cb) | 3.15 – 4.15 | Phosphorus | 0.015 max |
| Iron | 5.0 max | Sulfur | 0.015 max |
| Aluminium | 0.40 max | Cobalt (if determined) | 1.0 max |
Composition consistent with the N06625 limits of ASME SB-444 Table 2, which defines the same alloy.
| Parameter | Range |
|---|---|
| Nominal size | DN15 – DN600 (NPS 1/2" – 24") |
| Wall thickness | SCH 5S, 10S, 40S, 80S, 160, XXS |
| Socket bore | To ASME B16.11, machined to suit pipe OD/tolerance |
| Forming route | Seamless pushing (DN ≤ 600) or plate forming/welding (DN > 600 or non-standard) |
| Ends | Bevelled to ASME B16.25, plain ends optional |
Fittings are supplied solution annealed and pickled, with a bright annealed or pickled surface as required. Each fitting carries heat number, grade, standard, size, heat treatment condition and our works mark. Export packing in wooden cases or steel pallets with plastic end caps.
Send the grade, fitting type, nominal size, schedule, quantity and any third-party inspection requirement to our technical sales desk. We will confirm dimensional tolerance, delivery condition and the applicable ASME line item, and quote FOB Shanghai or Ningbo.
Socket weld is normally chosen for sizes DN50 and below where the pipe cannot easily be bevelled or where the joint must be made without a dedicated welding crew. For larger sizes, butt weld is stronger and more economical because it removes the joint gap and filler metal.
Grade 1 gives higher strength and suits most chemical service up to about 593°C. Grade 2 is solution annealed for better creep and rupture resistance and is normally specified above 593°C.
Yes. Where the service requires it, we can supply hardness records and control the condition to the NACE MR0175 / ISO 15156 limits. State this on your enquiry.
Yes, as standard on every fitting, with third-party inspection available on request.