Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
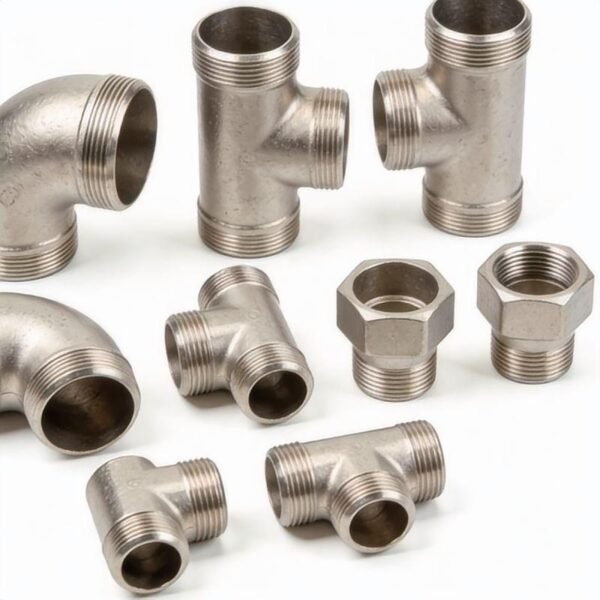
Inconel 625 UNS N06625 butt and socket weld fittings in Grade 1 and Grade 2 to ASME SB-366. Different anneal cycles, different tension test rules.
Inconel 625 (UNS N06625) carries two distinct mechanical property grades under ASME SB-366, and the difference between them is not cosmetic. Grade 1 is annealed at a lower temperature and retains higher strength and hardness; Grade 2 is annealed at a higher temperature for maximum corrosion resistance and ductility. Specifying “625” without the grade leaves the heat treatment open, which in turn leaves the certificate ambiguous and the weld procedure unqualified. This page exists so that buyers can order the correct grade deliberately.
45°, 90° and 180° elbows, equal and reducing tees, concentric and eccentric reducers, caps and lap-joint stub ends to ASME B16.9; socket weld and threaded fittings to ASME B16.11. Both grades supplied solution annealed with bevelled ends. Companion pipe to SB-444 and flanges to SB-462 / ASME B16.47 are available.
| Grade | UNS | Solution anneal | Quench |
|---|---|---|---|
| Grade 1 | N06625 | 1600 °F [871 °C] | Rapid air/water |
| Grade 2 | N06625 | 2000 °F [1093 °C] | Rapid air/water |
Both grades carry the same fitting class designation, CRNCMC / WPNCMC, and the same Ni-Cr-Mo-Cb composition. Only the heat treatment and its consequences differ.
The two grades do not carry the same testing burden, and this is where specification errors surface:
– Grade 1: tension tests are required per lot, per furnace charge. Specimens may be taken from a fitting or a representative test piece. For welded-construction fittings the specimen must include the weld, positioned at the specimen mid-length.
– Grade 2: tension tests are not required provided the starting raw material is designated UNS N06625 Grade 2 in the manufacturer’s MTR and the final heat-treatment temperature complies with the recommended solution annealing procedure. Tests are required if the incoming raw material is designated Grade 1.
In short: a Grade 2 fitting can legitimately ship with no new tensile test, provided the parent material certificate says Grade 2. A Grade 1 fitting cannot. If your project specification requires tensile testing regardless of grade, state so and we will perform and report it.
Per §7.1.2.4 and §7.1.3.4, finished fittings must conform to the mechanical properties of their respective starting raw material product — with one exemption common to both grades: fittings of welded construction are exempt from the elongation and yield-strength requirements. This matters when comparing a seamless fitting against a fabricated one on a datasheet; the strength columns are not directly comparable.
Grade 1 suits higher-strength, wear and impact-sensitive service — springs, fasteners, heavily loaded components and cryogenic service where the lower anneal preserves toughness. Grade 2 suits maximum corrosion resistance: seawater, sour gas, chemical processing, and high-temperature oxidation service where the upper anneal maximises grain-boundary cleanliness.
EN 10204 3.1 as standard, 3.2 on request, with PMI, tensile and hardness testing available. Every certificate states the grade explicitly and the heat-treatment temperature applied.
Specify grade (1 or 2), NPS size, wall thickness or schedule, quantity, end preparation and certification. If you are not sure which grade you need, tell us the service media, temperature and whether weld procedure qualification is in scope — we will recommend one and confirm before production.